
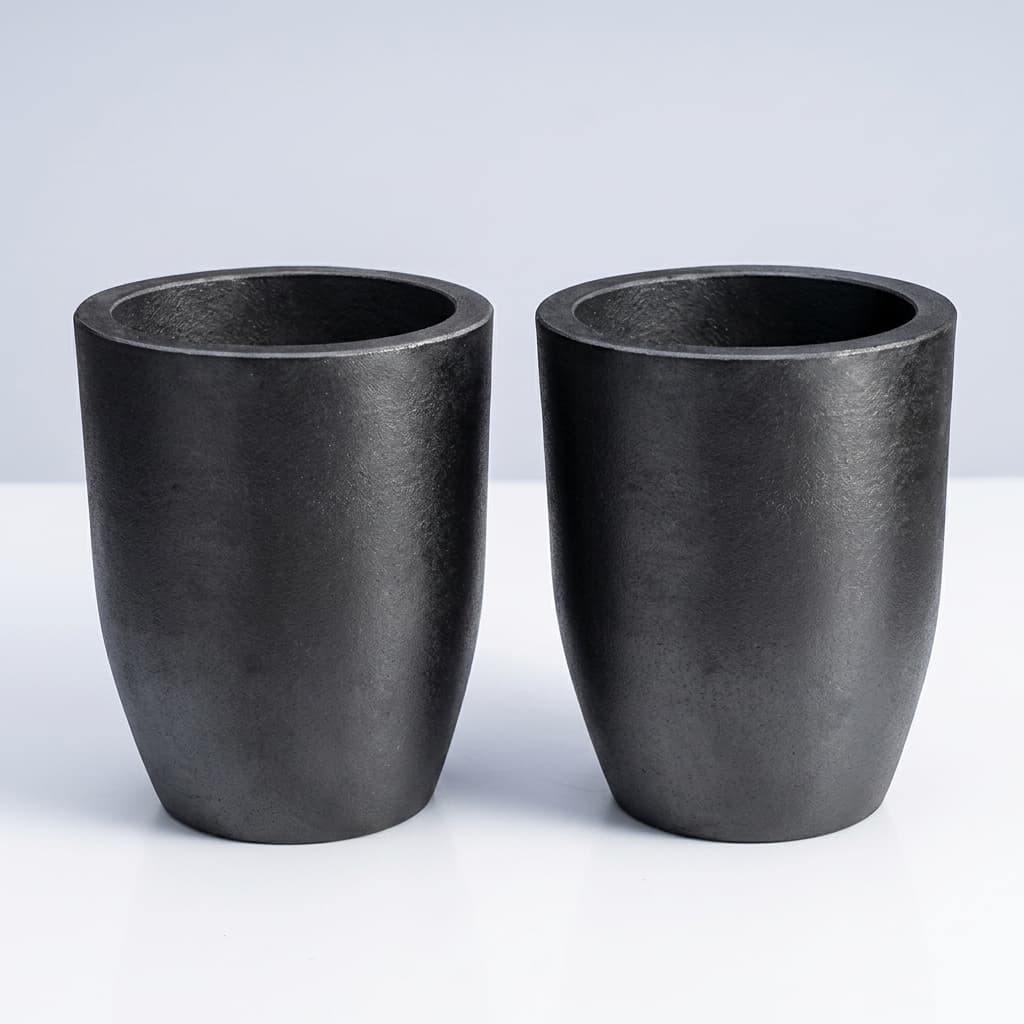
Graphite Crucible Lifecycle Management: Balancing TCO and Yield in SiC PVT
Graphite crucible lifecycle management framework for SiC PVT teams balancing TCO, replacement timing, power drift, and yield risk in production plants.
For procurement teams and facility managers overseeing Silicon Carbide (SiC) Physical Vapor Transport (PVT) facilities, the graphite crucible is one of the most expensive and critical consumables on the balance sheet. In the highly competitive 150mm and emerging 200mm SiC wafer markets, every decision revolves around reducing the cost per wafer while maintaining defect-free crystal growth.
This creates an inherent tension between procurement and engineering. Procurement wants to maximize the number of runs per crucible to amortize its high initial cost and improve Total Cost of Ownership (TCO). Meanwhile, process engineers recognize that as a crucible ages, its thermal and chemical properties degrade, leading to compromised thermal gradients, an unstable growth front, and ultimately, lower crystal yield. Pushing a crucible for "just one more run" to save a few thousand dollars can result in the catastrophic loss of a SiC boule worth ten times that amount.
This evergreen guide provides a data-driven framework for graphite crucible lifecycle management. By understanding the physical mechanisms of degradation, implementing a rigorous replacement cycle, and utilizing structured TCO modeling, operations can find the optimal balance between maximizing consumable life and protecting SiC crystal yield.
Published and scope note (July 26, 2026): This guide is written for global procurement, facility, and process engineering teams managing 150 mm and 200 mm SiC PVT graphite crucible programs. It is a lifecycle decision framework, not a universal run-count specification; thresholds such as power drift, weight delta, density, and ash targets must be qualified against each furnace design, recipe, coating route, source powder, and acceptance plan.
If you are mapping an RFQ or replacement trial, use this article with the SiC PVT Crucible requirements page so geometry, material grade, coating route, and inspection records are reviewed as one lifecycle system.
The Physical Realities of Crucible Aging
Unlike standard metallurgical crucibles, the graphite hot zone in a SiC PVT reactor does not simply "wear out" mechanically; it undergoes a complex evolution at temperatures exceeding 2,200°C. Three primary mechanisms drive the degradation of isostatic graphite during the sublimation process, each impacting the crucible's viability in different ways.
1. Silicon Vapor Infiltration and Corrosion
During the PVT process, the SiC source powder at the bottom of the crucible sublimes into complex vapor species, primarily Si, Si2C, and SiC2. The internal walls of the crucible are continuously bombarded by these vapors. Isostatic graphite, even high-density grades, contains inherent microporosity. Silicon vapor infiltrates these pores and reacts with the carbon matrix to form secondary SiC within the crucible wall.
According to research on the microstructural evolution of isotropic graphite under silicon vapor infiltration [1], this corrosion severely restricts service life. The formation of SiC in the pores reduces the available carbon, alters the chemical balance (the crucial C/Si ratio), and creates localized stress concentrations due to the coefficient of thermal expansion (CTE) mismatch between the newly formed SiC and the surrounding graphite matrix. Over multiple runs, this leads to micro-cracking and eventual structural failure during the cool-down phase.
2. Evolving Graphitization Degree
Graphite used in PVT systems starts with a specific "graphitization degree"—a measure of how perfectly the carbon atoms are arranged in a hexagonal lattice. Studies have demonstrated that the graphitization degree of a crucible changes over repeated high-temperature runs [2].
As the crucible is exposed to 2,300°C run after run, its crystalline structure continues to evolve. An increase in graphite crystallite size (higher graphitization) leads to a decrease in electrical resistivity and an increase in thermal conductivity [3].
3. Thermal Conductivity Drift and Gradient Collapse
The most insidious failure mode of an aging crucible is not catastrophic cracking, but thermal drift. The PVT process relies entirely on a precise axial temperature gradient (typically 20-30°C/cm) to drive sublimation from the powder to the seed.
As the crucible's graphitization degree increases and its thermal conductivity changes, the insulating properties of the hot zone are compromised. The heat generated by the induction coils transfers differently through an old crucible compared to a new one. The simulation results reveal that the whole temperature field and axial temperature gradient in the crucible are degraded significantly [3]. This causes the crystal growth rate to slow down and increases the probability of forming polytype inclusions (like 15R) or severe basal plane dislocations.
The TCO vs. Yield Paradox
To optimize lifecycle management, we must quantify the Total Cost of Ownership (TCO). A common mistake in procurement is calculating TCO based solely on the purchase price divided by the number of successful runs.
Flawed TCO Calculation:
Cost per Run = (Crucible Purchase Price) / (Number of Runs Achieved)
This formula ignores the cost of a failed run. In SiC PVT, a failed run means the loss of the high-purity SiC source powder, the argon gas, the electricity, the machine time, and the seed crystal—not to mention the lost revenue from the unyielded boule.
Correct TCO Calculation (Yield-Adjusted):
True Cost per Good Boule = (Crucible Price + Sum of Operating Costs for N runs) / (Number of High-Yield Boules)
Figure 1: The theoretical TCO curve. Pushing beyond the sweet spot causes the cost of yield degradation (red) to outpace the savings of hardware amortization (blue).
As the graph illustrates, there is a theoretical "sweet spot" where the crucible cost is sufficiently amortized, but the probability of a yield-destroying defect is still low. Operating beyond this vertical line is gambling with highly expensive inputs.
Establishing a Qualification and Retirement Strategy
So, how do operators determine when a crucible has reached the end of its useful life before a catastrophic failure occurs? Standardizing the replacement cycle requires strict empirical tracking.
Below is a comparative breakdown of how engineering and procurement teams should align their metrics to define the lifecycle.
| Metric / Indicator | Engineering Perspective | Procurement Perspective | Lifecycle Implication |
|---|---|---|---|
| Wall Thickness / Weight | Indicates Si vapor corrosion and SiC formation in pores. | Easily measurable KPI for consumable tracking. | Replace if weight increases by >X% (depends on crucible size) indicating severe vapor infiltration. |
| Heater Power Output | Need to supply more power to maintain 2,300°C due to altered thermal conductivity. | Higher electricity costs; indicates component wear. | Replace if power setpoint drifts beyond 5-8% of baseline recipe. |
| Boule Shape / Convexity | Loss of radial gradient causes flat or concave growth fronts, leading to stress. | Direct correlation to lower usable wafer yield per boule. | Replace immediately if growth front shifts away from desired convexity. |
| Nitrogen Doping Uniformity | Changes in crucible reactivity affect C/Si ratio, altering dopant incorporation. | Wafers fail resistivity specs, resulting in unsalvageable scrap. | Warning sign; usually mandates retirement for production runs (can be relegated to dummy runs). |
| Visual Micro-Cracking | Structural integrity compromised; high risk of catastrophic failure during cooling. | Immediate risk of losing expensive seed, powder, and production time. | Replace immediately. Never reuse a crucible with visible thread or wall hairline cracks. |
| Graphitization Degree (XRD) | Change in crystallite size alters thermal profile significantly. | Lab testing required, useful for lot qualification. | Replace based on batch-tested limits established during initial R&D. |
The "When to Retire" Checklist for Operations
To operationalize the lifecycle management, implement a strict go/no-go checklist between every run. If a crucible fails any of the following checks, it must be retired from standard production:
- Weight Delta: Is the crucible's post-run weight within the acceptable variance limit established during qualification? (Significant weight gain implies heavy SiC formation in pores).
- Thread Integrity: Can the lid be screwed on and off smoothly without excessive torque or grinding? (Thread seizure is a leading cause of boule loss).
- Visual Inspection: Are there zero visible hairline cracks under high-intensity inspection light, particularly around the crucible radius and threading?
- Previous Run Data: Did the previous run maintain the target heating power within a 5% tolerance band of the standard recipe?
- Yield Feedback: Did the previous boule exhibit the required convex growth front and acceptable basal plane dislocation (BPD) counts?
- Run Counter Limit: Has the crucible exceeded the strict empirical limit of runs defined by the engineering team for this specific boule diameter (e.g., maximum 5 runs for a specific 200mm design)?
Strategies to Extend Reliable Lifespan
While pushing a degraded crucible is dangerous, optimizing the hot zone to safely increase the baseline number of runs is a highly effective procurement strategy.
- Invest in Ultra-High Density Isostatic Graphite: Procurement should specify bulk densities of >1.85 g/cm³. Lower porosity directly resists silicon vapor infiltration, slowing down the structural degradation and thermal drift.
- Consider TaC Coatings: Tantalum Carbide (TaC) coatings act as a dense physical barrier against silicon vapor. TaC-coated crucibles resist graphitization changes and maintain stable thermal conductivity for significantly more runs. While the upfront cost is higher, the TCO can be substantially lower due to extended life and improved yield consistency.
- Optimize Cool-Down Profiles: A significant percentage of crucibles are destroyed not by the growth process, but by thermal shock during cooling. Programming slower, more controlled cool-down profiles minimizes the CTE mismatch stress between the solidified boule and the crucible walls.
- Use High-Purity Graphite Consumables: Ensure the graphite meets stringent GDMS purity standards. Impurities in the crucible not only affect the SiC crystal but can also accelerate localized degradation of the graphite matrix itself.
Frequently Asked Questions (FAQ)
Q: Can we use a fixed "number of runs" to determine when to replace our crucibles? A: While a fixed run limit is a safe administrative control, it is often suboptimal. A crucible might last 4 runs in one recipe and 7 in another. A data-driven approach based on power drift, weight changes, and crystal yield is far more accurate for balancing TCO.
Q: Why does the furnace require more power as the crucible ages? A: As the crucible is repeatedly exposed to extreme temperatures, its graphitization degree increases, which raises its thermal conductivity. Additionally, silicon vapor infiltration changes the material's properties. These factors degrade the thermal field, requiring the induction coils to work harder (consume more power) to maintain the required internal sublimation temperatures.
Q: Are there different replacement cycles for 150mm vs. 200mm crucibles? A: Yes. 200mm (8-inch) crucibles have larger surface areas, thicker walls, and experience substantially higher mechanical stress during cool-down due to the massive CTE forces of the 8-inch boule. Typically, 200mm crucibles face a more conservative replacement cycle than 150mm crucibles to prevent catastrophic failure.
Q: How does ash content relate to crucible lifespan? A: High ash content (impurities like V, Ti, Fe) doesn't just contaminate the crystal; these metallic impurities can catalyze localized degradation in the graphite under PVT conditions. Specifying ultra-high purity graphite (<5 ppm ash, verified by GDMS) ensures consistent degradation profiles.
Conclusion
Managing the lifecycle of a SiC PVT graphite crucible requires moving beyond a simple "cost per part" mentality. By understanding the physical degradation mechanisms—such as vapor infiltration and thermal conductivity drift—engineering and procurement can align on a TCO model that prioritizes crystal yield.
Implementing a strict qualification checklist and monitoring parameters like power drift and boule shape will prevent catastrophic failures while maximizing safe consumable usage.
To explore high-density isostatic graphite options tailored for extended lifespans in both 150mm and 200mm SiC PVT systems, review our SiC PVT Crystal Growth Solutions or contact our engineering team to discuss custom crucible geometries and TaC coating options designed to optimize your TCO.
Sources and References
Author
Categories
More Posts
Managing Silicon Vapor Leakage in SiC PVT: Sealing Strategies for Graphite Crucibles
Use this RFQ guide to manage silicon vapor leakage in SiC PVT graphite crucibles with density, thread tolerance, labyrinth seal, and TaC coating checks.
Isostatic Graphite Grain Size for SiC Crucibles: Balancing Machinability, Strength, and Yield
Evaluate isostatic graphite grain size for SiC PVT crucibles, from CNC thread integrity to TaC coating fit, thermal shock trade-offs, and RFQ checks.
Evaluating Graphite Crucible Porosity and Density for SiC PVT Growth
Use density and porosity limits to qualify SiC PVT graphite crucibles, control vapor penetration, reduce impurity risk, and compare supplier datasheets.